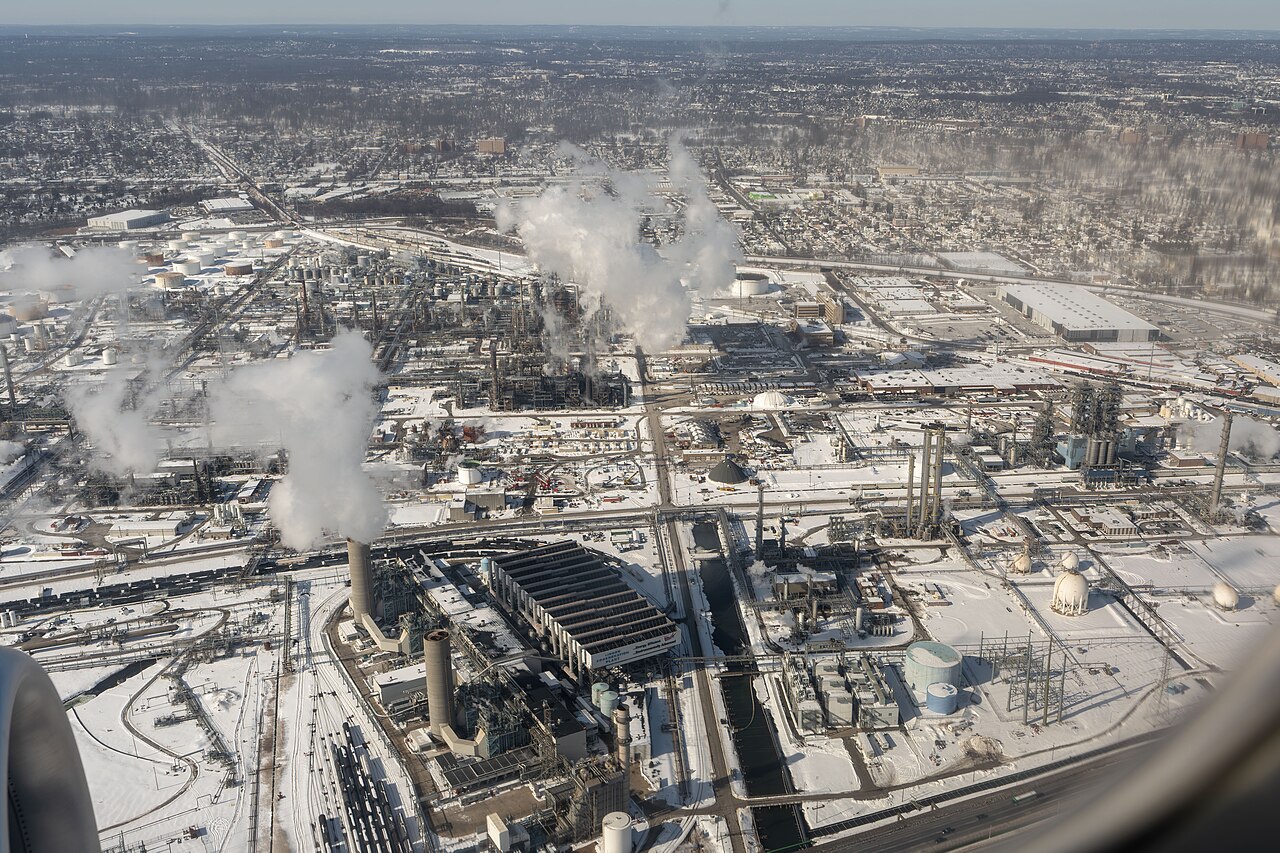
The fluid catalytic cracking (FCC) unit converts vacuum gas oil and, in residue units, part of the residue into LPG, gasoline and light cycle oil. Hot catalyst from the regenerator meets the feed at the bottom of a riser, cracks it in a few seconds, is separated and stripped, then returns to the regenerator where the coke deposited on it is burned. The heat from that coke drives the whole unit. This guide works through yields, the riser heat balance, riser sizing, the regenerator and catalyst metals with one synthetic 60,000 BPSD example.

1. Chemistry and yields
Cracking on the acid sites of Y zeolite proceeds through carbocations: they isomerize towards branched structures and break by beta-scission, which favours C3 and C4 olefins and branched gasoline-range molecules. Hydrogen transfer reactions convert olefins and naphthenes into paraffins and aromatics and contribute to coke. Secondary cracking of gasoline into gas becomes important at high severity.
Synthetic yields (wt% of feed): dry gas 3.0, LPG 16.0, gasoline 48.0, light cycle oil 18.0, slurry oil 10.0, coke 5.0. Yields must close to 100%; conversion, defined here on a weight basis as 100 minus LCO and slurry, is 72 wt%. Feed: 60,000 BPSD at 900 kg/m³ = 99.4 kg/s, or 8,585 t/day.
2. Riser heat balance and catalyst-to-oil ratio
Regenerated catalyst at 710°C supplies the heat to raise the feed from its preheat temperature (assumed 250°C) to vapor at the riser outlet temperature (530°C) and to drive the endothermic cracking reactions. With assumed properties (liquid cp 2.8 kJ/kg/°C to 400°C, vaporization 215 kJ/kg, vapor cp 2.9 kJ/kg/°C, heat of cracking 180 kJ/kg):
qfeed = 2.8 × 150 + 215 + 2.9 × 130 + 180 = 1,192 kJ/kg; CTO = 1,192 / (1.09 × (710 − 530)) ≈ 6.1
The catalyst-to-oil ratio (CTO) is therefore an outcome of the heat balance, not an independent choice. The delta coke, the coke laid down per pass, is the coke yield divided by CTO: 5.0 / 6.1 = 0.82 wt% of catalyst.
3. Riser size: the vapor is cracked
Riser volume must be calculated with the cracked products, which have far more moles than the feed. From the yields above, plus 3 wt% dispersion and stripping steam, the vapor at the outlet has an average molecular weight of about 79. At 2 bar absolute and 530°C its density is 2 × 10⁵ × 79.3 / (8,314 × 803) = 2.38 kg/m³, and the flow is about 41.0 m³/s. At 15 m/s the riser needs 2.73 m², a diameter of about 1.9 m; a 3-second vapor residence time gives a length of the order of 45 m. Using the feed molecular weight (about 180) would give 18.4 m³/s and an undersized 1.3 m riser.
4. Regenerator: the unit burns the coke the heat balance needs
Coke of composition CH0.9 contains 93.0 wt% carbon and 7.0 wt% hydrogen. Burned completely to CO2 and water vapor:
Q = 0.930 × 32.76 + 0.070 × 119.9 ≈ 38.8 MJ/kg coke; O2 needed ≈ 3.03 kg/kg coke; air with 10% excess ≈ 14.4 kg/kg coke
At 5.0 wt% coke (4.97 kg/s) the release would be 193 MW, with about 71 kg/s of air. But the heat actually needed is only what the circulating catalyst gives up in the riser (604 kg/s × 1.09 × 180°C ≈ 118 MW) plus the heating of the air to regenerator temperature (about 40 MW from an assumed 200°C), roughly 158 MW. In full-combustion operation, that corresponds to a coke yield of only about 4.1 wt%. A real unit cannot keep making more coke than its heat balance accepts: regenerator temperature rises, CTO falls and conversion drops until coke production matches the heat demand, unless the unit has a catalyst cooler or runs in partial combustion (burning part of the carbon only to CO, which releases less heat). This self-adjustment is the central idea of FCC operation.
5. Catalyst metals
Nickel promotes dehydrogenation (more hydrogen and coke); vanadium attacks the zeolite and causes permanent activity loss. At steady state, the metal on the equilibrium catalyst (E-cat) equals the metal deposited per day divided by the fresh catalyst added per day.
Synthetic case: feed with 1.2 ppm Ni and 2.1 ppm V deposits 10.3 kg Ni and 18.0 kg V per day. With a fresh catalyst addition of 0.15 lb per barrel of feed (about 4.1 t/day, an assumed rate), E-cat Ni ≈ 10.3 / 4,082 ≈ 2,500 ppm and V ≈ 4,400 ppm. With an unrealistically low addition of 0.5 t/day the same formula would give about 20,600 ppm Ni, which is why addition rate must be stated before drawing conclusions about feed quality. Antimony-based passivation for nickel, vanadium traps and metal-tolerant catalysts are the usual mitigations.
6. Raising riser outlet temperature: who pays?
Assume a 10°C higher outlet temperature shifts yields by +0.3 dry gas, +0.8 LPG, +0.5 gasoline and +0.3 coke, taken from −1.2 LCO and −0.7 slurry (wt% of feed). With assumed values of $800/t gasoline, $550/t LPG, $650/t LCO, $450/t slurry and $300/t for dry gas used as fuel, the change is about −$14,000 per day: the extra conversion loses money because LCO is worth more than the gas and coke made in its place. With a low LCO value or high LPG demand the answer reverses. Severity decisions must value every product, including those that decrease, and respect regenerator, wet gas compressor and air blower limits.
7. Feed quality
- Carbon residue and density: heavier, more aromatic feeds make more coke and less gasoline, and raise regenerator temperature.
- Metals: raise catalyst consumption or require passivation.
- Sulfur: appears in gasoline, LCO and flue gas SOx. Where gasoline is limited to 10 ppm sulfur, FCC feed hydrotreating and/or selective gasoline hydrotreating are needed.
- Nitrogen: basic nitrogen neutralizes acid sites and lowers conversion.
References
- R. Sadeghbeigi, Fluid Catalytic Cracking Handbook, 4th ed. (Butterworth-Heinemann, 2020)
- J.H. Gary, G.E. Handwerk and M.J. Kaiser, Petroleum Refining: Technology and Economics. Heats of combustion from standard enthalpies of formation
Related reading and community
Questions or field experience to share? Join the PetroSmart Telegram group, watch worked examples on the PetroSmart Academy YouTube channel and follow us on Facebook.